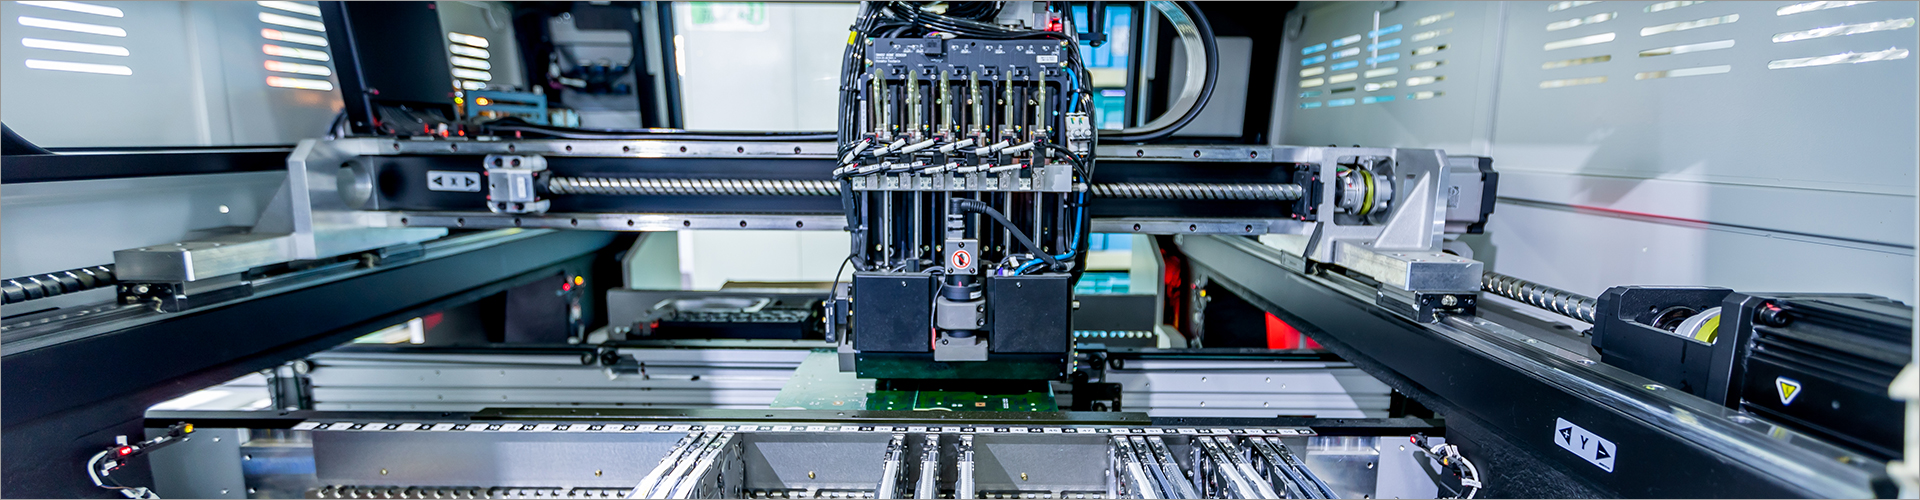
To select a product inspection unit for a production line, start with the defect or product characteristic you need to detect, then match the inspection method to your line speed, product presentation, environment, and acceptance criteria. A suitable unit should inspect products consistently at the required throughput and provide a clear way to handle failed or uncertain results. Before comparing suppliers, document the product, target defects, inspection location, and how the unit must communicate with your existing equipment. This guide explains the main options and gives buyers a practical framework for evaluating fit.
Please visit our website for more information on this topic.
This guide is for production engineers, quality managers, automation integrators, and purchasing teams sourcing an inspection system for a new or existing line. It is relevant when you need to check product presence, appearance, dimensions, weight, assembly features, or other measurable characteristics. The appropriate solution depends on the product and inspection task, so a system suitable for one line may not suit another. Use the selection steps below to turn your quality requirement into a supplier-ready specification.
A product inspection unit is equipment installed at a defined point in a production process to assess products against specified criteria. Depending on its design, it may use cameras, sensors, scales, measurement devices, or a combination of methods. The unit can identify results for downstream actions, such as accepting a product, triggering a reject mechanism, or recording an inspection outcome. Its capabilities should be defined by the checks it must perform, rather than by the general label “inspection unit.”
These functions are not interchangeable. For example, a camera-based unit may be appropriate for checking label position, while a dimensional measurement may require suitable optics, calibration, and a controlled product position. Some applications combine methods, but added functions can affect system complexity, setup, and validation. Ask suppliers to explain how each required check will be performed and what conditions can affect the result.
Begin with representative samples of both acceptable products and known defect conditions. Record product variations such as color, finish, packaging, orientation, and changes between batches, because these can affect sensing or image-based inspection. Define the defect size or condition that must trigger a failure decision, and state whether the system should identify a specific defect or simply flag a nonconforming product. If defects cannot be reproduced reliably, discuss how the supplier will evaluate samples and agree on test criteria.
Measure the actual line rate and identify whether products arrive with consistent spacing and orientation. As an illustrative requirement, a buyer might specify a rate of 120 units per minute; this is an example for documenting a project, not a performance claim for any particular unit. The supplier should assess the full operating cycle, including sensing, decision processing, communication, and reject timing. Also consider whether inspection occurs before or after packaging, at a transfer point, or in an area where products may move unpredictably.
Describe relevant site conditions, including dust, moisture, vibration, washdown practices, available space, and operator access. Provide details of the conveyor, controls, and existing automation, then confirm the required signal exchange and safe response when a product fails inspection. Ask how the system will stop or flag the line if inspection data is unavailable, and how operators will distinguish a confirmed defect from a system fault. Integration requirements should be reviewed with the equipment supplier and the team responsible for the line controls.
Yinglai Technology Product Page
Do not use a single headline specification as a substitute for an application review. A stated measurement resolution, camera specification, or maximum line rate does not by itself demonstrate that a system will detect the defect you care about on your product. Ask for the assumptions behind any proposed capability, including product positioning, lighting, sample condition, and inspection recipe. Where possible, have the supplier assess representative samples and record the agreed test conditions.
The project price depends on the inspection method, number of checks, mechanical arrangement, controls integration, guarding, and any custom fixtures or software configuration. A standard configuration may differ in scope and cost from a system designed around a specific product or line, so compare quotations by deliverables rather than total price alone. Ask whether installation, commissioning, training, documentation, and future product recipes are included or quoted separately. For an eight-hour shift, for example, a buyer should clarify how recipes, changeovers, and routine checks will fit into the operating schedule; this is a planning example, not a claimed inspection duration.
Minimum order quantity and lead time depend on the supplier’s equipment model, component availability, customization, and project scope. Request a written schedule that identifies design approval, sample evaluation, production, shipment, installation, and commissioning milestones where applicable. Also ask how design changes after approval may affect cost or delivery. Yinglai Technology can review the application requirements and discuss the appropriate product configuration, customization scope, and supply details with buyers.
Evaluate suppliers on the evidence and clarity they provide, not on broad claims of suitability. A useful proposal should connect each requirement to a proposed inspection method and identify any limitations or assumptions. If two quotations use different test conditions or define different included equipment, request clarification before comparing them. This reduces the risk of selecting a low-cost system that does not cover the actual production need.
One frequent mistake is choosing a unit based only on the product category without defining the defect or measurement. Another is specifying the nominal line speed but overlooking spacing variation, product movement, or changeovers. Buyers may also assume that every fault will result in automatic rejection, even when the proposal does not include a reject mechanism or the required control interface. Make each of these requirements explicit and confirm them in the technical scope.
A further risk is treating sample testing as proof of every possible production outcome. Samples can help evaluate a defined application, but testing conditions should reflect the real product range and operating environment as closely as practical. Agree on the sample set, pass/fail criteria, and method for recording results. If production conditions change later, review whether the inspection setup still meets the requirement.
The right product inspection unit is the one that addresses a clearly defined quality check while fitting the line’s speed, products, environment, and integration needs. Begin by listing the features or defects to inspect, then document acceptance criteria, operating conditions, and the required response to failed results. Compare supplier proposals against this specification and verify capability using representative samples where practical. As a next step, prepare product details, defect examples, line information, and interface requirements, then share them with Yinglai Technology to discuss a suitable inspection solution and project scope.
For more information, please visit Product Inspection Unit.
2
0
0
All Comments (0)
Previous: None
Next: Steel Ladle Refractory Lining Machine: A Buyer’s Selection Guide
If you are interested in sending in a Guest Blogger Submission,welcome to write for us!

Comments